Controlling heat, movement and low-surface-energy interfaces

Polypropylene Sheet Fabrication: Machining, Welding and Surface Control

Polypropylene sheet fabrication turns solid PP into panels, dividers, liners, trays and fabricated equipment components. Reliable results depend on identifying the exact PP construction, carrying chips and heat away during cutting, allowing for directional and thermal movement, and qualifying every welded, printed or bonded interface.

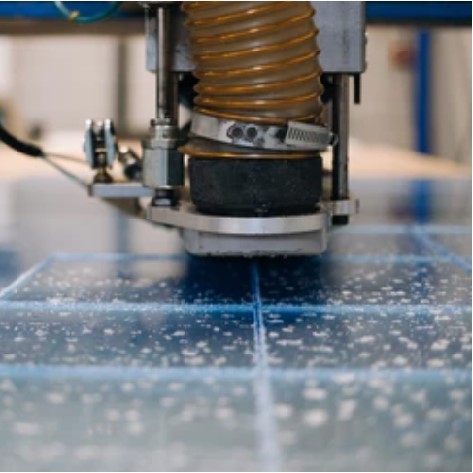
Solid polypropylene sheet prepared for controlled cutting and fabrication
Material scopeSolid PP sheet with an identified grade, surface and direction
Core processesSaw, CNC, drill, qualify laser, bend, weld, print and inspect
Quality focusEdge condition, free-state dimensions, joint function and adhesion

Project logic

Make the process fit the product.

01

Identify the PP construction before choosing a process

PP sheet is a material family, not a complete specification. Homopolymer, block copolymer and random copolymer products can be supplied with fillers, conductive or antistatic modifications, backing, flame modification or surface treatment. The record for a fabrication job should identify the approved grade or supplier reference, nominal thickness, colour, texture, treated or backed face, visible face and extrusion direction. It should also identify the later cutting, heating, welding, printing, chemical exposure and mechanical fastening steps. Food-contact, flame, ESD, chemical or other regulated requirements belong to the exact grade documentation and finished application; they cannot be assigned to generic PP. Store sheet flat and supported, away from uneven heat, direct sunlight and dust, because a bowed or locally warmed blank can make later process results inconsistent.

02

Plan flat and finished datums as one fabrication route

The route should follow the finished part rather than a list of available machines. A flat divider may need cutting, holes and deburring. A printed folder adds treated-side control and an adhesion check after folding. A welded tray needs compatible sheet and filler, prepared seams, controlled assembly and a functional joint test. A formed shell needs heating, cooling and trim datums planned together. Define which features are created while flat and which are finished after bending or welding. A hole can move relative to a flange after heating, graphics can cross a bend or weld zone, and a part trimmed before it is dimensionally stable can drift later. Approve dimensions in the free state unless the drawing deliberately defines a restrained condition.

03

Saw, route and mill while carrying heat away in the chip

SIMONA and Röchling both support conventional sawing and machining of PP with sharp suitable tools, stable support and effective chip removal. The objective is a continuous cut without a smeared, rolled or heavily burred edge. Support flexible sheet close to the cut, use adequate swarf space and clear chips before they rub or weld back onto the edge. CNC routing and milling can produce profiles, pockets, slots and trim features, but workholding should not crush the sheet or force a bowed blank flat. Thin walls may deflect under the tool and spring back after release. Qualify the actual geometry because corners, narrow slots, repeated passes and dwell can build more heat than a straight test coupon. Inspect the first-off part after it is unclamped.

04

Drill and fasten without binding, breakout or forced alignment

Drilling follows the same heat-and-chip logic. SIMONA notes that deep holes may require repeated withdrawal to remove shavings and that heat can make a large drill bind. Use a sharp tool, support the exit face and inspect for a raised lip, melt smear, tearing or breakout. Hole diameter, edge distance, bearing area and expected thermal movement should be reviewed together. A fastener should spread load without indenting a flexible wall, and the joint should permit the movement required by the design. Do not use bolts or screws to pull a misaligned PP panel into position: the assembly may look correct while storing load around the holes. Where location is critical, establish finished datums after bending or welding and check the released assembly.

05

Treat laser cutting as a material-and-equipment qualification

Trotec lists solid PP among materials that can be laser cut, and SIMONA lists laser cutting for a specific PP-H sheet. This supports feasibility, not a universal approval for every formulation. For a proposed laser route, verify the exact sheet and additives, equipment and extraction, protective masking, deposits, odour or discolouration, heat-affected edge and downstream bending, welding or load. Use representative production material and include a demanding feature from the actual profile. Compare the cooled edge with the drawing's cosmetic and functional requirements. If residue, edge condition or EHS acceptance is not documented, use a qualified mechanical cutting route. Generic laser settings from another PP grade or another plastic are not a responsible substitute for a production trial.

06

Control direction, heating, cooling and trim during forming

PP can be hot-line bent and can be thermoformed when the grade and equipment support the route. Its semi-crystalline behaviour makes heating and cooling part of the dimensional plan. SIMONA explains that shrinkage varies with material, batch, cooling, demoulding state, stretch, tooling and extrusion direction. For a line bend, heat the zone uniformly, bend in a defined fixture and hold it until the part is sufficiently stable. Record sheet direction because response can differ along and across extrusion. A full formed shape adds draw, radii, draft, clamping, venting, wall distribution, tool contact, cooling and final trim. Approve dimensions after a representative cooling interval. Wrinkles, thin areas, springback, unstable walls and asymmetric distortion are process evidence. Full-sheet PP thermoforming should only be offered when the specific project capability has been confirmed.

07

Match sheet, filler, joint design and inspection for welding

Thermoplastic welding is a documented joining route for compatible PP. Röchling states that the welding rod must match the material and that rod and joint surfaces must be clean. SIMONA adds that seam preparation, heating balance, cooling sequence and weld geometry influence distortion and joint quality. The drawing should identify the PP family on both parts, filler, joint type, load direction, tool access, restraint and inspection method. Keep print, oil, marker residue and unknown cleaning chemistry away from the weld zone. Plan the sequence so one side does not accumulate heat and pull the assembly out of square. A neat bead does not by itself prove joint strength or leak integrity. The acceptance method must match the finished function, and available welding equipment, operator qualification and test scope must be confirmed before they are promised.

08

Treat printing and adhesive bonding as qualified surface systems

Untreated PP has low surface energy, so many liquids do not wet it reliably. LyondellBasell explains that oil, slip and antistatic additives can affect printing and adhesion, that flame or corona treatment may modify the surface, and that treatment effectiveness can decline with time. SIMONA likewise treats untreated PP as difficult to glue and calls for suitable pretreatment or adhesives designed for low-energy surfaces. A surface-treated sheet therefore needs traceability for the treated side, treatment method or verification, storage interval, contamination controls and compatible ink or adhesive. Approve printing after the next operation—folding, flexing, cleaning or abrasion—not only while the sheet is flat. Adhesive bonding should remain a project-specific engineering route unless the substrate, preparation, adhesive instructions, cure, joint load, exposure and destructive validation have all been approved.

09

Use failure evidence and staged inspection to control quality

Incoming inspection confirms grade, supplier reference, surface, treatment or backing, direction, flatness and damage. After cutting and machining, check free-state dimensions, burr, smear, rewelded chips, edge deformation, hole condition and surface marks. After bending or forming, inspect the cooled shape, orientation, warpage, wall distribution and trim. Weld inspection covers material and filler identity, seam preparation, continuity, distortion and the specified functional test. Print or adhesive checks cover treated-side identity, contamination, cure and the relevant flex, rub, clean or exposure condition. Melt smear points toward poor heat or chip removal; a torn hole toward binding or lost exit support; twist after bending toward uneven heating, cooling or direction; print lift toward treatment, contamination or ink compatibility. These diagnostic principles come from SIMONA, Röchling, LyondellBasell and Trotec product guidance; their product-specific settings do not become universal PP values.

Applications

Where this route creates value.

01Cut PP panels and profiles
02Reusable dividers and partitions
03Industrial liners and guards
04Fabricated trays and vessels
05Printed and folded PP components
06Machined PP equipment parts

Common questions

Details buyers ask before an RFQ.

Can polypropylene sheet be CNC machined?+

Yes. Official sheet-manufacturer guidance supports sawing, routing, milling and drilling PP. Use sharp tooling, stable support and effective chip removal, then approve dimensions after the part is released.

Can PP sheet be laser cut?+

Selected solid PP sheets can be laser cut, but the exact grade, additives, equipment, extraction, masking, edge condition and downstream use need a representative material and equipment trial.

Can polypropylene sheet be bent without heat?+

Some designed PP products can flex or fold, but there is no universal cold-bend rule. Grade, thickness, extrusion direction, radius and repeated movement must be tested. Controlled hot-line bending is a separate route.

Is thermoforming the same as line bending PP?+

No. Line bending heats a local zone to create an angle. Thermoforming shapes a larger heated area against a tool, so draw, wall distribution, shrinkage, cooling and trim become part of the process.

Is welding better than adhesive bonding for PP?+

Welding is a documented PP joining route but still needs compatible material, joint design and qualified execution. A specialised adhesive may work after preparation, but it must be validated for the actual load and exposure.

Why can PP printing fail after first looking acceptable?+

Low surface energy, additives, contamination, treatment ageing, incompatible ink or insufficient cure can reduce adhesion. Test the actual treated sheet after expected folding, cleaning, flexing or abrasion.

What should a PP fabrication drawing identify?+

Identify the exact grade, thickness record, extrusion direction, treated and visible faces, flat and finished datums, joints, graphic zones, free-state dimensions, inspection priorities and packing orientation.